
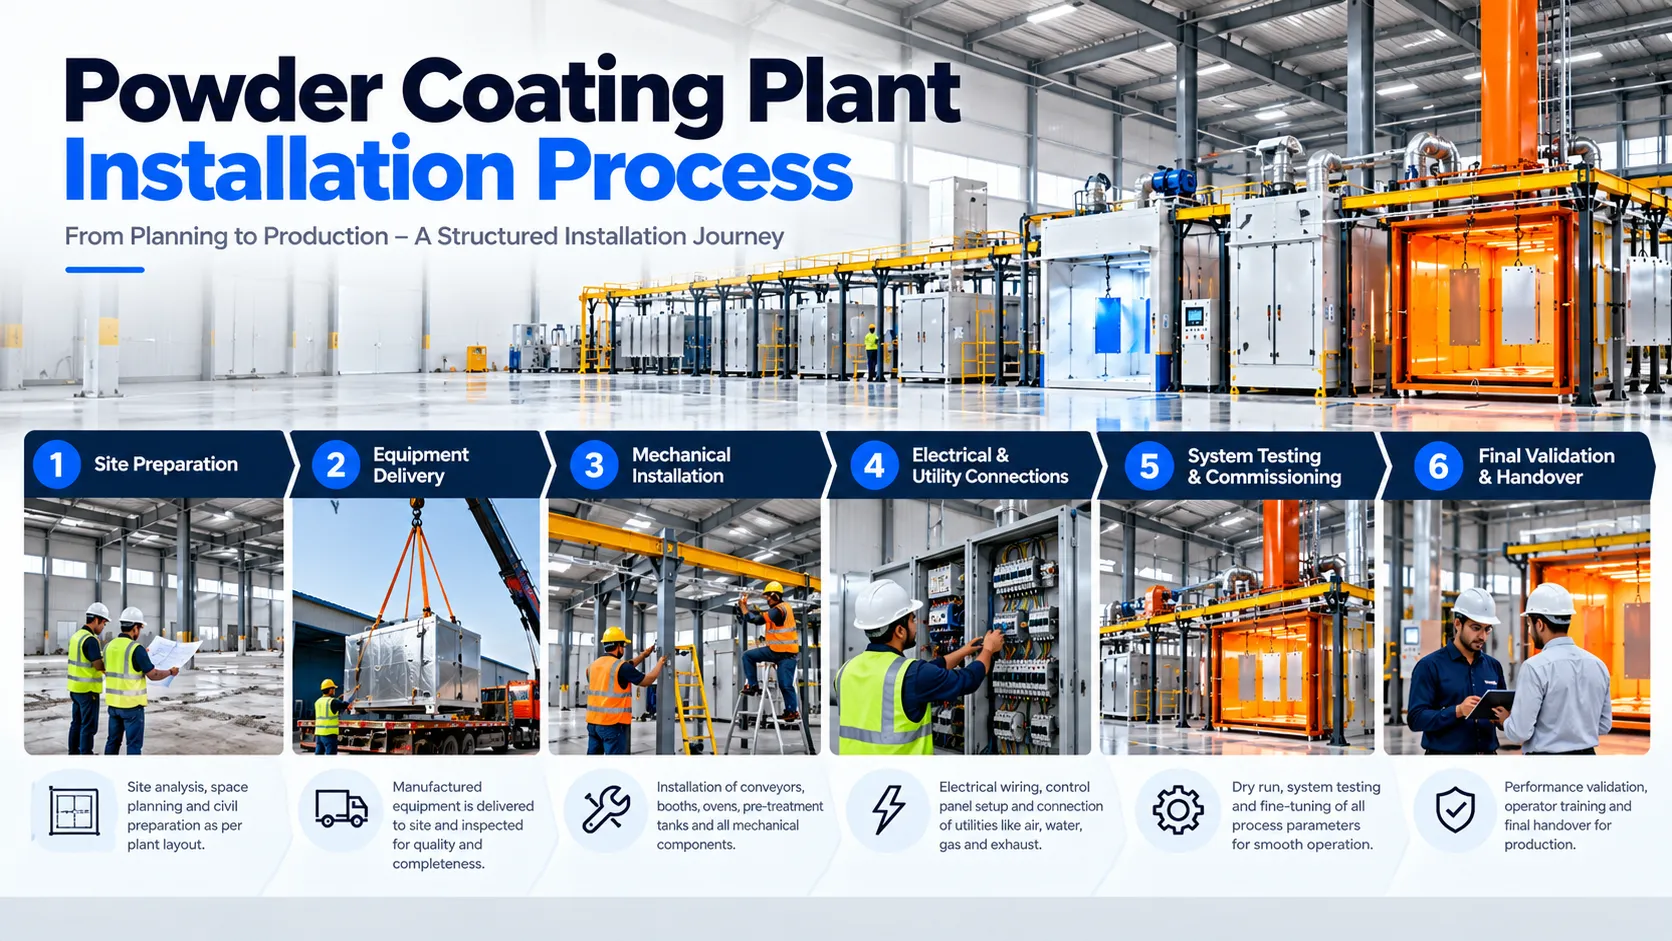
Installing a powder coating plant involves much more than positioning a booth, oven and conveyor inside a factory. A successful powder coating plant installation process begins with production requirements and factory readiness, then moves through mechanical erection, utility integration, testing, commissioning, operator training and final handover.
For a turnkey or conveyorised system, the complete process typically follows this sequence:
Requirement confirmation → layout approval → factory readiness → equipment delivery → mechanical installation → utility integration → pre-commissioning → dry trials → process commissioning → production trials → acceptance testing → operator training → documentation → handover
The important distinction is that installation and commissioning are not the same thing. Installation confirms that the equipment has been positioned and connected. Commissioning proves that the complete coating process can operate safely, consistently and according to the agreed production requirements.
Manufacturers planning a new line can review Brahma Fabricon’s powder coating plant solutions and powder coating projects and installations to understand how different plant configurations can be engineered around specific products and production requirements.
Powder Coating Plant Installation Process at a Glance
| Project Stage | Main Objective |
|---|---|
| Requirement confirmation | Freeze product, capacity and coating-process requirements |
| Layout approval | Confirm equipment positions, material flow and service clearances |
| Factory readiness | Prepare civil work, access, utilities and drainage |
| Equipment delivery | Receive, inspect and stage equipment for erection |
| Mechanical installation | Position and assemble the plant equipment |
| Utility integration | Connect electricity, compressed air, water, fuel and drainage |
| Pre-commissioning | Inspect each subsystem before powered trials |
| Dry commissioning | Test mechanical movement, controls and safety systems |
| Process commissioning | Establish pretreatment, powder application and curing conditions |
| Production trials | Coat representative customer components |
| Acceptance testing | Verify agreed performance and production criteria |
| Training | Prepare operators and maintenance personnel |
| Handover | Transfer documentation and the commissioned plant to production |
What Is the Powder Coating Plant Installation Process?
The powder coating plant installation process is the coordinated sequence used to prepare a manufacturing facility, install powder coating equipment, integrate utilities and controls, validate process performance and hand over a production-ready finishing system.
Depending on the project, the plant can include:
- pre-treatment tanks or spray tunnels;
- dry-off ovens;
- powder coating booths;
- cyclone or cartridge recovery systems;
- manual or automatic powder guns;
- reciprocators;
- powder feed and management systems;
- curing ovens;
- overhead, floor or power-and-free conveyors;
- PLC and HMI controls;
- ducting and ventilation;
- water and wastewater systems;
- loading and unloading stations.
A turnkey installation is successful only when these systems operate together as one controlled production process.
Installation vs Commissioning vs Handover
These three stages are closely connected but serve different purposes.
Installation
Installation involves physically positioning, assembling and connecting the plant equipment.
Typical installation activities include:
- equipment positioning;
- conveyor erection;
- oven assembly;
- booth installation;
- ducting;
- piping;
- electrical wiring;
- compressed-air connections;
- water and drainage connections;
- fuel connections.
Commissioning
Commissioning verifies whether the installed plant actually performs as intended.
It can include:
- conveyor trials;
- airflow verification;
- oven heating tests;
- temperature profiling;
- powder booth extraction testing;
- gun and reciprocator trials;
- pretreatment process checks;
- PLC and safety-interlock verification;
- actual workpiece coating trials.
Handover
Handover takes place after the agreed commissioning and acceptance activities have been completed. The operating team receives the plant, training and documentation required for routine production and maintenance.
Phase 1: Confirm Production Requirements Before Installation
The installation project should begin with a confirmed basis of design. Changing fundamental production requirements after equipment manufacturing has started can lead to expensive modifications.
Confirm Workpiece Information
Document the:
- minimum component dimensions;
- typical component dimensions;
- maximum component dimensions;
- maximum component weight;
- substrate;
- geometry;
- hanging orientation;
- masking requirements;
- coated surface area where relevant.
The complete hanging envelope—including the workpiece and fixture—should be considered when designing conveyor clearances, booth openings, pretreatment equipment and ovens.
Confirm Production Capacity
Define the expected:
- parts per hour;
- parts per shift;
- shifts per day;
- hanger pitch;
- parts per hanger;
- expected future production.
Confirm the Coating Specification
The project team should also confirm:
- pretreatment requirement;
- powder type;
- target film thickness;
- powder cure schedule;
- number of colours;
- colour-change frequency;
- customer or OEM quality specifications.
A line designed for lightweight sheet-metal cabinets will require different handling, curing and equipment sizing from a line intended for heavy CNC machine bodies or large fabricated structures.
Phase 2: Approve the Final Powder Coating Plant Layout
The approved plant layout should show much more than equipment footprints.
It should identify:
- loading area;
- conveyor route;
- pre-treatment equipment;
- dry-off oven;
- powder coating booth;
- powder recovery equipment;
- curing oven;
- cooling zone;
- inspection area;
- unloading area;
- operator access;
- maintenance access;
- electrical panels;
- utility termination points;
- powder storage;
- chemical storage;
- wastewater route;
- ETP connection;
- columns, doors and structural obstacles.
The layout should represent the plant’s working footprint, not only its machine footprint.
For detailed planning principles, see our guide to powder coating plant layout design.
Allow Space for Maintenance
A booth may physically fit into a space while still being difficult to maintain if there is no room to remove filters, service a cyclone or access automatic guns.
Similarly, ovens need access to:
- burners or heating elements;
- recirculation fans;
- motors;
- ductwork;
- sensors;
- control devices.
Service clearances should be included before the layout is frozen.
Phase 3: Define Customer and Supplier Responsibilities
Powder coating plant projects often involve interfaces between the equipment supplier, customer and third-party contractors. These responsibilities should be defined before equipment dispatch.
| Project Requirement | Responsibility to Define |
|---|---|
| Equipment manufacture | Supplier scope |
| Transportation | Customer or supplier |
| Unloading | Crane/forklift responsibility |
| Civil foundation | Customer or nominated contractor |
| Electrical incomer | Customer/supplier interface |
| Plant internal wiring | Define clearly |
| Fuel connection | Define termination point |
| Compressed air | Define pressure, quality and connection |
| Water supply | Define connection and quality |
| Drainage | Define interface |
| ETP | Define treatment and piping scope |
| Trial powder | Define responsibility |
| Pretreatment chemicals | Define responsibility |
| Trial components | Customer production samples |
A clear responsibility matrix reduces disputes and prevents the commissioning team from arriving at a factory where essential utilities are incomplete.
Phase 4: Prepare the Factory Before Equipment Delivery
A site is ready when equipment can be unloaded, positioned, connected and commissioned without unnecessary delays.
Check Factory Access
Verify:
- main gate dimensions;
- internal door dimensions;
- truck access;
- unloading area;
- crane capacity;
- forklift capacity;
- internal transport route;
- turning radius.
Large oven and pretreatment modules may fit comfortably once installed but can still be difficult to move through an existing factory.
Check Floors and Foundations
Confirm:
- floor condition;
- floor levels;
- equipment plinths;
- foundation positions;
- anchor points;
- required pits;
- drainage slopes.
Incorrect civil dimensions can cause alignment problems later, especially with conveyor systems.
Verify Clear Height
For overhead conveyor systems, consider the full vertical envelope:
floor clearance + workpiece + hanger/fixture + conveyor trolley/track + structural clearance
Measure the lowest actual obstruction—not simply the nominal roof height.
Phase 5: Prepare Electrical Infrastructure
The final plant load schedule should be reviewed before commissioning.
Electrical consumers may include:
- conveyor drives;
- pretreatment pumps;
- process heaters;
- booth extraction fans;
- recovery equipment;
- powder guns;
- reciprocators;
- oven circulation fans;
- electrical oven heating;
- PLC and HMI;
- lighting;
- ancillary equipment.
Confirm the available power supply, connected load, cable sizing, protection devices and earthing using the final equipment specification.
Phase 6: Prepare Compressed Air
Powder application depends on stable, clean compressed air.
Compressed air may operate:
- powder pumps;
- gun controls;
- fluidizing systems;
- pneumatic actuators;
- pulse-cleaning systems;
- control valves.
Before commissioning, verify:
- available pressure;
- airflow capacity;
- pipeline size;
- compressor capacity;
- receiver capacity;
- filtration;
- moisture removal;
- dryer requirements.
Contaminated or wet compressed air can interfere with powder transport and application consistency.
Phase 7: Prepare Water, Drainage and Wastewater Infrastructure
Plants using wet pretreatment need coordinated water and wastewater infrastructure.
Check:
- process-water supply;
- required water quality;
- tank filling;
- rinse-water arrangements;
- overflow management;
- floor drainage;
- wastewater segregation;
- ETP connection;
- sludge management.
The actual requirements depend on the pretreatment chemistry and local discharge requirements.
Brahma Fabricon’s pre-treatment plant systems include dip, spray and other configurations that can be integrated into complete powder coating lines.
Phase 8: Prepare Fuel and Oven Services
Gas-fired ovens may require:
- PNG, LPG or another specified fuel source;
- pressure-regulation equipment;
- isolation valves;
- gas train;
- burner controls;
- ventilation;
- exhaust;
- safety interlocks.
Electric ovens require adequate electrical infrastructure instead.
These utilities should be ready before final commissioning begins.
Manufacturers comparing curing options can review Brahma Fabricon’s powder curing ovens.
Phase 9: Receive and Inspect the Equipment
Equipment should be inspected immediately after arrival.
Verify:
- delivered quantity;
- equipment identification;
- visible transit damage;
- critical components;
- motors;
- fans;
- filters;
- burners or heaters;
- control panels;
- powder guns;
- conveyor components;
- accessories;
- documentation.
Missing or damaged components should be documented before installation progresses.
Phase 10: Mechanical Installation of the Powder Coating Plant
Mechanical erection should follow the approved general arrangement and supplier drawings.
A typical conveyorised plant may be assembled in this general order:
support structures → main process equipment → conveyor → ducting → process piping → access platforms → utilities → controls
The actual installation sequence depends on building access and project design.
Installing the Pre-Treatment Plant
For a spray pretreatment system, installation can include:
- spray tunnel;
- chemical tanks;
- pumps;
- spray headers;
- nozzles;
- filters;
- heating;
- process piping;
- drainage.
For a dip system, equipment can include tanks, transfer systems, circulation equipment, heating, exhaust and drainage.
Installing the Dry-Off Oven
Verify:
- chamber alignment;
- panel joints;
- insulation;
- air circulation;
- heating system;
- conveyor clearances;
- service access.
Installing the Powder Coating Booth
Booth installation can include:
- booth enclosure;
- extraction system;
- cartridge filters or cyclone recovery;
- after-filter;
- powder management equipment;
- manual or automatic guns;
- reciprocators;
- ducting.
For booth-selection considerations, see our industrial powder coating booth guide.
Installing the Curing Oven
Verify:
- chamber assembly;
- insulation;
- burner or heater installation;
- recirculation fans;
- ductwork;
- exhaust;
- control sensors;
- conveyor openings;
- maintenance access.
Phase 11: Install and Align the Conveyor
The conveyor connects the major process stages and should be aligned carefully.
Check:
- support positions;
- track level;
- track alignment;
- curves;
- drive assembly;
- take-up/tensioning;
- chain lubrication;
- hanger clearance;
- oven entry and exit;
- loading height;
- unloading height.
During initial running, watch for:
- binding;
- excessive vibration;
- unexpected noise;
- workpiece collisions;
- excessive swinging;
- clearance problems.
For high-volume lines, review Brahma Fabricon’s conveyorised powder coating plant systems.
Phase 12: Complete Piping, Ducting and Utility Connections
After the main equipment is positioned, complete the interfaces for:
- compressed air;
- process water;
- drainage;
- fuel;
- exhaust;
- electrical power;
- control wiring;
- sensors.
Pipes, valves and service points should remain accessible for routine inspection and maintenance.
Phase 13: Integrate PLC, HMI, Drives and Sensors
Automated powder coating plants may use a PLC/HMI to coordinate:
- conveyor speed;
- pretreatment pumps;
- oven temperatures;
- booth fans;
- automatic guns;
- reciprocators;
- alarms;
- emergency-stop circuits;
- safety interlocks.
Each input and output should be tested individually before complete automatic operation is attempted.
Typical I/O Verification
A simple verification sequence is:
sensor changes condition → PLC receives signal → programmed action occurs → HMI displays the correct state
This helps identify wiring, sensor and programming issues before production trials.
Phase 14: Verify Grounding and Earthing
Effective grounding is critical to electrostatic powder application and plant safety.
Inspect:
- booth grounding;
- conveyor grounding;
- hanger contact;
- workpiece grounding;
- electrical continuity;
- powder buildup on fixtures.
The U.S. Occupational Safety and Health Administration’s spray finishing requirements provide a useful technical reference for grounding and ventilation principles. The final installation should comply with the standards and statutory requirements applicable to the actual factory location.
Phase 15: Conduct Pre-Commissioning Checks
Pre-commissioning confirms that each subsystem is mechanically complete and ready for powered testing.
| System | What to Check |
|---|---|
| Conveyor | Alignment, lubrication, clearances and tension |
| Pretreatment | Pumps, tanks, piping, heaters and nozzles |
| Powder booth | Filters, airflow path, ducting and grounding |
| Recovery system | Cartridges/cyclone, seals and connections |
| Powder guns | Air, controls and electrical connections |
| Ovens | Fans, heating, sensors and exhaust |
| Electrical | Terminations, protection and earthing |
| Compressed air | Pressure, quality and leaks |
| PLC/HMI | I/O, alarms and communications |
| Safety | E-stops and interlocks |
Phase 16: Perform Dry Commissioning
Dry commissioning tests the equipment before normal coating production begins.
Conveyor Trial
Run the conveyor through the expected operating range and check:
- movement;
- chain tension;
- clearances;
- turns;
- loading stations;
- equipment entry and exit.
Airflow Trial
Verify:
- booth extraction;
- recovery airflow;
- oven circulation;
- exhaust performance.
Control-System Trial
Test:
- start and stop sequences;
- alarms;
- permissives;
- emergency stops;
- drive controls;
- HMI status information.
Heating Trial
Bring the oven through controlled heating cycles while checking:
- temperature control;
- fan operation;
- heater or burner response;
- alarms;
- unexpected heat loss.
Phase 17: Commission the Pre-Treatment Process
The pretreatment process should be established using the chemical supplier’s documented operating conditions.
Depending on the process, commissioning can include checking:
- bath concentration;
- pH;
- temperature;
- spray pressure;
- contact time;
- rinse quality;
- nozzle coverage;
- drainage;
- chemical carryover.
Do not copy chemical operating values from another coating plant. Pretreatment should be established for the actual substrate, contamination level, chemistry and required coating performance.
Phase 18: Commission the Powder Coating Booth
Powder application trials should begin after booth airflow, grounding and compressed air have been stabilized.
Verify:
- powder containment;
- booth extraction;
- automatic gun triggering;
- powder flow;
- reciprocator movement;
- recovery operation;
- reclaim where applicable.
Develop Product Recipes
Actual product trials can then be used to optimize:
- voltage and current;
- powder flow;
- air settings;
- gun distance;
- gun angle;
- reciprocator stroke;
- line speed;
- manual touch-up.
The objective is to establish a repeatable coating condition—not merely to achieve visual coverage on one component.
Phase 19: Commission and Profile the Curing Oven
One of the most important commissioning activities is verifying the actual temperature experienced by the workpiece.
The temperature shown on the oven controller is not automatically the same as the temperature of the metal component.
The Powder Coating Institute’s technical guidance explains that powder coating cure depends on achieving the required metal temperature for the specified time.
Use Actual Production Components
Where appropriate, temperature sensors or a profiling system can be attached to representative areas such as:
- thick sections;
- thin sections;
- top surfaces;
- bottom surfaces;
- shielded sections;
- areas expected to heat slowly.
The resulting temperature profile should be compared with the powder manufacturer’s technical data.
Why Thermal Mass Matters
A thin sheet-metal panel can reach its required metal temperature much faster than a heavy fabricated frame.
Two parts can therefore pass through the same oven at the same air temperature but experience very different actual curing conditions.
Phase 20: Run Actual Production Components
Commissioning should ultimately use representative production parts rather than relying only on simple test panels.
Useful trial components can include:
- the maximum-size component;
- the heaviest component;
- a typical high-volume component;
- a product with complex geometry;
- a component with recesses;
- a product requiring masking.
These trials help reveal whether the plant performs correctly under actual factory conditions.
Phase 21: Validate Production Capacity
The plant should meet both quality and throughput requirements.
For a conveyorised line:
Theoretical parts per hour = conveyor travel per hour ÷ hanger pitch × parts per hanger
However, real output can also be affected by:
- loading speed;
- empty hangers;
- pretreatment dwell;
- powder application;
- colour changes;
- curing;
- unloading;
- maintenance;
- rejects.
The slowest effective production stage becomes the line bottleneck.
Phase 22: Complete Acceptance Testing
Acceptance criteria should ideally be agreed before equipment installation starts.
| Area | Possible Acceptance Criterion |
|---|---|
| Material handling | Maximum agreed component moves safely |
| Conveyor | Agreed operating-speed range |
| Pretreatment | Required process stages operate correctly |
| Booth | Effective powder containment and extraction |
| Application | Representative parts receive repeatable coverage |
| Curing | Actual part profile meets powder requirements |
| Film thickness | Within agreed specification |
| Appearance | Meets agreed finish standard |
| Output | Meets agreed production basis |
| Controls | PLC, HMI and alarms function correctly |
| Safety | Defined interlocks function correctly |
| Documentation | Required project documents supplied |
A measurable acceptance standard is more useful than simply stating that the plant should “work properly.”
Phase 23: Resolve Problems Identified During Commissioning
Commissioning exists partly to identify issues before normal production begins.
| Problem | First Areas to Investigate |
|---|---|
| Uneven coating | Gun position, grounding, airflow |
| Powder escaping booth | Extraction and airflow balance |
| Poor recessed coverage | Gun settings, electrostatics and geometry |
| Water remaining on parts | Drainage and dry-off process |
| Poor adhesion | Cleaning, pretreatment and cure |
| Under-cure | Part temperature, conveyor speed and oven profile |
| Colour contamination | Booth and recovery-system cleaning |
| Components colliding | Hanger pitch and conveyor movement |
| Low throughput | Loading, process dwell or curing bottleneck |
Troubleshooting should identify the process stage responsible for the defect rather than repeatedly adjusting whichever machine is easiest to access.
Phase 24: Train Production and Maintenance Teams
A commissioned plant still needs trained operators.
Production Training
Operators should understand:
- start-up;
- shutdown;
- loading;
- hanger positioning;
- masking;
- recipe selection;
- powder gun operation;
- colour change;
- basic process checks;
- alarms;
- emergency stops.
Maintenance Training
Maintenance personnel should understand:
- preventive-maintenance intervals;
- filter replacement;
- booth cleaning;
- powder gun wear parts;
- conveyor lubrication;
- fan maintenance;
- burner/heater inspection;
- pump and nozzle maintenance;
- sensor troubleshooting;
- electrical safety.
Training should occur during commissioning whenever possible so operators see how real production settings are developed.
Phase 25: Complete Final Handover
The handover package should give the manufacturer enough information to operate and maintain the plant after the installation team leaves.
Depending on the agreed project scope, documentation may include:
- final plant layout;
- equipment drawings;
- electrical drawings;
- utility information;
- control-system information;
- operating manuals;
- maintenance schedules;
- recommended spare-parts list;
- equipment datasheets;
- warranty documentation;
- commissioning records;
- temperature-profile records where included;
- operator-training records.
The exact handover requirements should be defined in the project scope.
Powder Coating Plant Factory Readiness Checklist
| Readiness Requirement | Status |
|---|---|
| Final layout approved | □ |
| Equipment access route clear | □ |
| Floor/foundations complete | □ |
| Required drains/pits complete | □ |
| Clear height verified | □ |
| Electrical supply ready | □ |
| Earthing available | □ |
| Fuel supply available | □ |
| Compressed air ready | □ |
| Process water available | □ |
| Drainage/ETP ready | □ |
| Exhaust route available | □ |
| Crane/forklift available | □ |
| Powder available for trials | □ |
| Pretreatment chemicals available | □ |
| Representative products available | □ |
| Acceptance criteria approved | □ |
How Long Does Powder Coating Plant Installation Take?
There is no universal installation timeline.
Project duration depends on:
- plant size;
- equipment configuration;
- conveyor length;
- pretreatment complexity;
- oven size;
- automation;
- factory readiness;
- utility availability;
- building access;
- amount of site fabrication;
- commissioning scope;
- production-trial requirements.
A manual batch plant and a fully automated conveyorised line should not be assigned the same installation schedule.
A useful project schedule separates:
site preparation → equipment delivery → erection → utility integration → pre-commissioning → process trials → acceptance → handover
What Commonly Delays Powder Coating Plant Installation?
Common causes include:
- factory foundations not ready;
- layout changes after equipment manufacture;
- inadequate electrical capacity;
- fuel connection incomplete;
- compressed air unavailable;
- drainage unfinished;
- ETP not ready;
- factory access too small;
- trial powder unavailable;
- pretreatment chemicals unavailable;
- representative components unavailable;
- customer and supplier scopes unclear;
- required approvals incomplete.
A detailed pre-installation readiness review can prevent many of these problems.
Common Powder Coating Plant Installation Mistakes
Starting Installation Before the Layout Is Frozen
Late changes can create rework in conveyor routing, piping, electrical cabling and equipment foundations.
Treating Utilities as a Later Activity
A mechanically complete plant cannot be fully commissioned if power, compressed air, water, drainage or fuel are missing.
Ignoring Maintenance Access
Tightly packed equipment may reduce floor area but increase future downtime when filters, pumps, burners or motors cannot be reached easily.
Starting Production Immediately After Mechanical Erection
Mechanical completion does not prove process stability. Dry and process commissioning should occur first.
Testing Only Easy Components
Maximum-size, heavy or difficult parts can expose problems that simple test panels do not.
Using Oven Air Temperature as the Only Cure Check
Actual component temperature and required time at temperature determine whether the powder receives the intended cure.
No Written Acceptance Criteria
The customer and supplier may otherwise have different definitions of successful commissioning.
Insufficient Operator Training
The plant may perform correctly during supplier trials but deteriorate after handover if production and maintenance teams do not understand the system.
Who Should Be Involved in Powder Coating Plant Installation?
A successful project can involve:
- plant/project management;
- production;
- maintenance;
- electrical engineering;
- utility engineering;
- EHS/safety;
- quality;
- powder supplier;
- pretreatment chemical supplier;
- equipment supplier;
- installation contractors.
For larger projects, civil, fire, gas and statutory specialists may also need to participate.
Why Real Powder Coating Plant Project Experience Matters
The installation stage is where engineering drawings meet real factory conditions.
Actual installations have to accommodate:
- building columns;
- roof beams;
- crane paths;
- component handling;
- operator movement;
- existing utilities;
- production schedules.
Brahma Fabricon’s powder coating project portfolio includes installations and applications involving conveyorised plants, aluminium sections, automobile components, cleanroom panels, control panels, cylinders and other industrial finishing requirements.
Reviewing relevant project examples can help manufacturers discuss the practical aspects of:
- equipment layout;
- plant scale;
- material handling;
- conveyor configuration;
- booth arrangements;
- factory integration.
What Information Should You Send Before Installation Planning?
| Requirement | Information to Provide |
|---|---|
| Factory layout | CAD/PDF with dimensions |
| Clear height | Lowest usable factory height |
| Columns | Locations and sizes |
| Access | Door and gate dimensions |
| Components | Photos and drawings |
| Maximum part | L × W × H and weight |
| Typical production | Product mix |
| Required output | Parts/hour or shift |
| Substrate | MS, aluminium, GI, etc. |
| Pretreatment | Required process |
| Powder | Product and cure schedule |
| Colours | Number and frequency |
| Electricity | Supply and available load |
| Fuel | PNG/LPG/electric/etc. |
| Compressed air | Capacity and quality |
| Water | Availability and quality |
| Drainage | Existing arrangement |
| ETP | Existing or proposed |
| Acceptance | Required performance tests |
Frequently Asked Questions About Powder Coating Plant Installation
What is the first step in powder coating plant installation?
The first step is to confirm the production requirements, equipment scope, final layout and customer/supplier responsibilities. Physical installation should begin only after the factory area and agreed utility interfaces are ready.
What factory utilities are required for a powder coating plant?
Requirements can include electricity, compressed air, water, drainage, fuel, exhaust and wastewater treatment. The exact requirements depend on the pretreatment plant, powder booth, oven, conveyor and automation level.
Should the factory be ready before the equipment arrives?
Yes. Access routes, foundations, civil work and agreed utility interfaces should ideally be complete before equipment delivery so installation can begin without avoidable delays.
What is the difference between installation and commissioning?
Installation involves positioning and connecting the equipment. Commissioning verifies the complete integrated plant, tests controls and process conditions, runs representative components and confirms whether the agreed performance requirements have been achieved.
How is a powder coating curing oven commissioned?
The oven is checked mechanically and electrically, then operated through controlled heating cycles. During process commissioning, representative components should be temperature-profiled to confirm that their actual metal temperature satisfies the powder manufacturer’s specified cure schedule.
Why is oven temperature profiling important?
Oven air temperature does not necessarily equal component temperature. Different materials, section thicknesses and component masses heat at different rates, so profiling the workpiece provides better evidence that the coating has received the required cure.
What components should be used during commissioning trials?
Use representative production components. Where appropriate, include the largest part, heaviest part, high-volume product and a component with difficult geometry so the plant is tested under realistic production conditions.
What should be checked during conveyor commissioning?
Check track alignment, chain movement, tension, lubrication, operating speed, hanger clearances, bends, process-equipment entry and exit points and loading/unloading positions.
When should operators be trained?
Operators should be involved during commissioning so they can learn the plant while actual process settings are developed. Formal production and maintenance training should be completed before final handover.
What documents should be provided at plant handover?
Depending on the project scope, the handover package may include final drawings, operating manuals, electrical information, maintenance schedules, spare-parts recommendations, commissioning records, warranty information and training documentation.
How long does powder coating plant commissioning take?
There is no universal duration. It depends on plant complexity, automation, factory readiness, pretreatment chemistry, production trials, product variety and how quickly any issues found during commissioning can be corrected.
What are the most common causes of commissioning problems?
Common causes include unstable pretreatment, poor grounding, incorrect booth airflow, incomplete drying, unsuitable application settings, incorrect conveyor speed and inadequate curing. Troubleshooting should identify the root process stage rather than treating every visible coating defect as a powder gun problem.
Conclusion
The powder coating plant installation process should be managed as a complete engineering project rather than simply an equipment erection activity.
A reliable project sequence is:
requirements → layout → factory readiness → installation → utilities → controls → pre-commissioning → dry trials → process commissioning → actual-part trials → acceptance → training → handover
The most important work often starts before the equipment reaches the factory.
An approved layout, adequate site access, completed civil work, suitable utilities and clearly defined responsibilities can prevent many installation delays.
After erection, commissioning should demonstrate more than whether individual machines start and stop. The complete plant should prove stable material handling, pretreatment, drying, powder application, recovery, curing, controls and agreed safety functions using representative production components.
Only after those stages are completed is the plant ready to transition from an installation project into a production system.
Brahma Fabricon provides integrated powder coating plant solutions for different manufacturing requirements. Manufacturers planning a new installation can also review the company’s completed powder coating projects to explore applications across conveyorised plants, control panels, aluminium sections, automobile components, cleanroom panels, cylinders and other industrial products.